How to Design an Injection Mold?

Designing an injection mold is not simply a matter of shaping a cavity around a part. It means coordinating geometry, material behavior, machine limits, cooling, and ejection so production can be consistent. David Kazmer, a professor and author of Injection Mold Design Engineering, has written extensively on the relationship between mold design and manufacturing performance. A concise paraphrase of his approach is: “Treat the mold as part of the process, not just as a cavity.” That distinction matters.

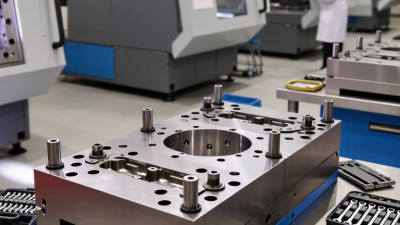
A sound design begins with the part: its wall thickness, ribs, bosses, expected shrinkage, and visible surfaces. These details influence the parting line, draft angles, gate location, and ejection strategy. Cooling channels also deserve early attention. A steel mold may look balanced on a drawing, yet uneven cooling can leave a real part warped near a thick boss. Small decisions accumulate. The mold should be checked against the chosen resin, expected cycle time, machine platen, and maintenance needs—not only the CAD model.

There is no universal layout. A gate that fills one material well may create weld lines or poor appearance with another. Simulation can reveal likely pressure and temperature patterns, but it cannot replace material data, toolmaking experience, or trial parts. And the first design may be wrong. That is worth admitting. This guide explains how to develop an injection mold design, review its key features, and refine it before steel is cut.
How to Design an Injection Mold?

Define Part Requirements and Select a Suitable Plastic

Before choosing a resin, write down what the part must survive: load, impact, temperature, chemicals, sunlight, and expected service life. Add the real operating details. A clip inside a warm appliance faces different demands from a clear outdoor cover. Specify critical dimensions, surface finish, color, and assembly method too. Small details matter. A tight snap-fit may need toughness, while a thin rib demands reliable flow into the cavity. Check the selected grade’s datasheet for melt flow, shrinkage, and drying requirements; these values vary between grades, even within one polymer family. A common shop-floor miss is treating “plastic” as one material. It is not.

Production and end-of-life also deserve attention. PlasticsEurope’s Plastics – the Fast Facts 2024 report estimated global plastics production at 413.8 million tonnes in 2023. That scale makes material choice consequential, but it does not make one resin universally preferable. OECD’s Global Plastics Outlook reported that only 9% of plastic waste was recycled in 2019.

Where recycled content is considered, test its effect on color, strength, and process consistency against the part’s requirements. Not just strength.

I would also review the mold design with the resin in mind: wall thickness, flow paths, gate location, and expected shrinkage can all affect fit. The uncomfortable truth is that early requirements are often incomplete; record assumptions and revisit them after prototype testing.

Analyze Part Geometry for Moldability and Defect Risks

Part geometry controls how resin fills, cools, and releases from the mold. Review wall thickness across the entire CAD model, not only at the main body. A 2 mm panel meeting a 4 mm boss can cool unevenly, leaving sink marks or internal voids. Smooth thickness transitions help. Small details matter. Ribs should support the part without creating thick, slow-cooling intersections. Keep them thinner than the adjoining wall where practical, and check their height against the part’s stiffness needs. Add draft to vertical faces so the part can eject cleanly; even a small angle can reduce drag and surface scuffing.

Trace likely material flow from the gate through narrow passages and around holes. Where flow fronts meet, weld lines may form, sometimes near visible or highly loaded areas. Gate placement and venting affect these risks, so geometry should be reviewed alongside the proposed mold layout. Look for undercuts, deep pockets, and features that may require side actions. They are not automatically defects, but they add tooling complexity and can constrain design changes. It is easy to overvalue perfectly uniform walls; some parts need local reinforcement. Treat that choice as a trade-off, then validate critical areas with mold-flow analysis or trial parts. A simulation can guide decisions, but it cannot replace checking real surfaces and dimensions.

How to Design an Injection Mold: Draft Angle and Surface Texture

Draft helps a molded part release from the mold. As surface texture becomes deeper, more draft is generally needed to reduce drag and the risk of scuffing or sticking. These are common starting-point guidelines, not universal requirements; resin, texture depth, part geometry, and mold finish can change the appropriate angle.

Choose the Mold Layout, Cavity Count, and Parting Line

How to Design an Injection Mold?
Choose the Mold Layout, Cavity Count, and Parting Line

Start with the part’s shape, material, and expected production volume. These choices guide the mold layout: a two-plate mold may suit a straightforward part, while complex geometry can require slides or lifters. Keep the cavity near the center when practical, and balance runner lengths so resin reaches each cavity under similar conditions. Small details matter. Gate access and cooling channels need room, too.

Cavity count is a production decision, not a race to fit in more parts. Grand View Research’s Injection Molded Plastics Market Size report valued the global market at USD 330.41 billion in 2023 and projected a 5.1% compound annual growth rate from 2024 to 2030. That scale makes efficient tooling important, but a higher cavity count can raise tool cost and make filling balance harder. Match the count to demand, press capacity, and acceptable cycle time. A simple fill analysis can expose imbalance before steel is cut.

Place the parting line where the mold can open cleanly and eject the part without damaging visible surfaces. A line around a sharp corner may leave a noticeable witness mark; a line across a sealing face can create extra finishing work. Check draft, undercuts, and shutoff areas together, not one at a time. I still recheck the parting line after layout changes; a tidy drawing can hide a poor release path.

How to Design an Injection Mold? - Choose the Mold Layout, Cavity Count, and Parting Line

Use these planning guidelines to compare mold layouts. Final decisions depend on part geometry, resin, production volume, machine capacity, tolerances, and tooling budget.

Design Factor Common Options Selection Guidance Benefits and Trade-Offs Typical Application
Mold layout Two-plate mold; three-plate mold; hot-runner mold Choose a two-plate layout for a straightforward parting surface and conventional gating. Consider a three-plate layout when gate location or automatic gate separation warrants the extra mechanism. A hot runner can reduce runner scrap but adds system cost and control requirements. Two-plate designs are generally simpler to build and maintain. Three-plate and hot-runner layouts can improve gate placement or material efficiency, but increase complexity and initial cost. Two-plate: many general-purpose parts. Three-plate: applications needing a separate gate location. Hot runner: sustained production where reduced runner waste can justify the investment.
Cavity count Single-cavity; 2-, 4-, 8-, or higher-cavity mold Estimate required output from annual demand, cycle time, uptime, and available production hours. Confirm that the projected shot size, clamp force, tie-bar spacing, and mold dimensions suit the press. More cavities increase output per cycle, but typically raise tooling cost and make filling, cooling, ejection, and process control more demanding. A single cavity offers lower tooling complexity but lower output per cycle. Single cavity: prototypes, low-volume parts, or large components. Multi-cavity: repeat production of smaller parts when demand and machine capacity support it.
Cavity arrangement In-line; square or rectangular; circular; family mold Arrange identical cavities symmetrically around the sprue or runner where practical. For family molds, group different components only when their material, color, wall thickness, and processing requirements are compatible. A balanced arrangement can support more uniform filling and packing. Family molds can produce related parts in one cycle, but mismatched part sizes or flow requirements can make cavity balance and yield difficult. Symmetric layouts: multiple identical parts. Family molds: matched components that are used together and have compatible molding requirements.
Runner balance Geometrically balanced cold runner; naturally balanced runner; hot runner Design runner paths and gate sizes to deliver melt to cavities with comparable flow resistance. Validate the layout with mold-flow analysis when cavity count, geometry, or quality requirements make filling balance critical. Balanced filling helps reduce cavity-to-cavity variation in fill, packing, and part weight. Runner balancing can require additional analysis and careful tuning; a hot runner also requires temperature control. Multi-cavity molds, especially where consistent dimensions or part weight across cavities are important.
Parting-line location Perimeter split; stepped or contoured split; parting line on a broad face Place the parting line where it is practical to separate the part from the mold and where any flash or witness mark is acceptable. Consider appearance, sealing surfaces, shutoffs, draft, and the direction of mold opening. A well-chosen line can simplify tooling and reduce visible defects. Complex contours or tight shutoffs may increase machining and maintenance demands; parting-line mismatch can affect appearance and fit. Choose a less-visible edge for appearance-critical parts when the geometry allows, while keeping functional interfaces clear of unwanted flash.
Parting direction and undercuts Straight-pull opening; side actions; lifters; collapsible cores Orient the part to release along the main mold-opening direction where possible. Use side actions or lifters only when features such as cross-holes or external undercuts cannot be redesigned or released by another practical method. Straight-pull designs are usually simpler and more robust. Slides, lifters, and collapsible cores enable additional geometry but add cost, moving components, and maintenance needs. Straight-pull: parts with suitable draft and no trapped features. Side actions or lifters: parts with unavoidable undercuts.
Draft and release Draft on core and cavity surfaces; textured-surface draft; local relief Specify draft in relation to wall depth, resin, texture, and ejection direction. Textured surfaces generally need more draft than smooth surfaces. Confirm draft and release conditions with the tooling and finishing teams. Adequate draft reduces drag, scuffing, and ejection force. Insufficient draft can cause sticking or surface damage; adding draft may affect appearance or fit and should be checked against functional requirements. Most molded surfaces benefit from draft; deep or textured walls need particular attention.
Gate location Edge gate; tab gate; fan gate; pin gate; hot-tip gate Locate gates to promote a suitable fill pattern and place gate vestige where it is acceptable. Consider weld-line position, air evacuation, cosmetic surfaces, wall thickness, and how the part will be packed. Gate choice affects filling, weld lines, vestige, and gate removal. A gate may leave a visible mark or require trimming; the best location depends on part geometry and resin behavior. Use a gate location that avoids critical cosmetic or sealing areas where feasible and supports reliable filling.
Venting and ejection Parting-line vents; ejector-pin vents; ejector pins; sleeves; stripper plate Provide vents near likely end-of-fill regions and arrange ejection so the part releases without distortion. Choose ejector locations on areas that can tolerate witness marks and withstand ejection loads. Effective venting helps reduce trapped-air defects and burning. Well-planned ejection supports consistent release; vent or ejector marks may be visible, so locations need to be coordinated with part appearance. All mold layouts; vent and ejection details should be reviewed alongside the predicted flow path and part geometry.

Design the Runner, Gate, Cooling, and Ejection Systems

How to Design an Injection Mold?

Design the Runner, Gate, Cooling, and Ejection Systems

A reliable mold depends on how its systems work together. The runner should deliver melt evenly, without unnecessary length or sharp turns. For a cold runner, estimate the material left in the runner against the part’s shot weight. A small part with a bulky runner can create avoidable scrap.

The gate location also matters: place it to support a balanced fill and reduce visible weld lines. Check the actual flow pattern; intuition alone can mislead.

Cooling deserves close attention. MoldMaking Technology’s technical guidance notes that cooling may take roughly 70–80% of an injection molding cycle. That makes channel layout a production decision, not just a machining detail. Keep channels near the cavity where steel thickness and strength allow, and check for hot spots around thick ribs and bosses. Measure part temperatures during trials. A neat-looking channel layout can still cool unevenly.

Ejection needs the same practical review: position pins beneath sturdy areas, then watch for whitening, drag marks, or distortion as parts release. Leave room for venting and maintenance access. Small compromises happen. Record them, and revisit them after the first mold trial.

Validate the Mold Design Through Simulation and Review

A simulation is useful only when its inputs resemble the real tool and material. Check the resin data, wall thickness, gate position, vents, and cooling layout before trusting the color plots. The fill study should reveal short shots, hesitation, air traps, and weld-line locations. Review those locations against appearance and strength requirements, not just the software’s pass/fail indicators. Small details matter.

PlasticsEurope’s Plastics – the Fast Facts 2024 reports that global plastics production reached 413.8 million tonnes in 2023. That scale makes repeatable mold performance important, but a digital result is not proof of production readiness. Compare predicted fill time, peak pressure, clamp force, and cooling behavior with trial measurements. Then review the results with the moldmaker, process engineer, and product designer. One overlooked vent can still cause burns. It happens.

Check warpage against the part’s critical dimensions, especially around ribs, bosses, and thick-to-thin transitions. If the model predicts distortion, test gate changes or cooling adjustments before cutting steel. Record assumptions and unresolved risks in the review. Simulation can be wrong; material batches and machine settings vary. A practical design review leaves room for that uncertainty.