10 Rubber Injection Molding Tips for Global Buyers
For global buyers, sourcing rubber components is rarely just a price comparison. A part that looks simple on a drawing can behave differently after curing, trimming, and repeated use. Rubber injection molding can produce consistent shapes at useful volumes, but results depend on the fit between the material, mold, and application. That fit takes evidence.
Before approving a supplier, buyers should clarify the rubber grade, operating temperature, expected load, and critical dimensions. Ask how the supplier controls curing time, injection pressure, and batch variation. Request samples, inspection records, and clear answers about tooling ownership and maintenance. A polished quotation is helpful, but it cannot replace a part tested under real conditions.
These ten tips cover supplier evaluation, material selection, mold design, quality checks, communication, and delivery planning. They are intended to make comparisons more practical, especially when teams work across time zones or use different technical terms. Small details matter: a sample label, a stated tolerance, or a photo of a mold cavity can prevent avoidable confusion. Still, no checklist removes every risk. Specifications may change, and not every supplier will explain limitations clearly. Buyers should leave room to question assumptions, verify claims, and revise decisions when test results disagree. That extra pause can be valuable.
Understanding Rubber Injection Molding and Its Applications
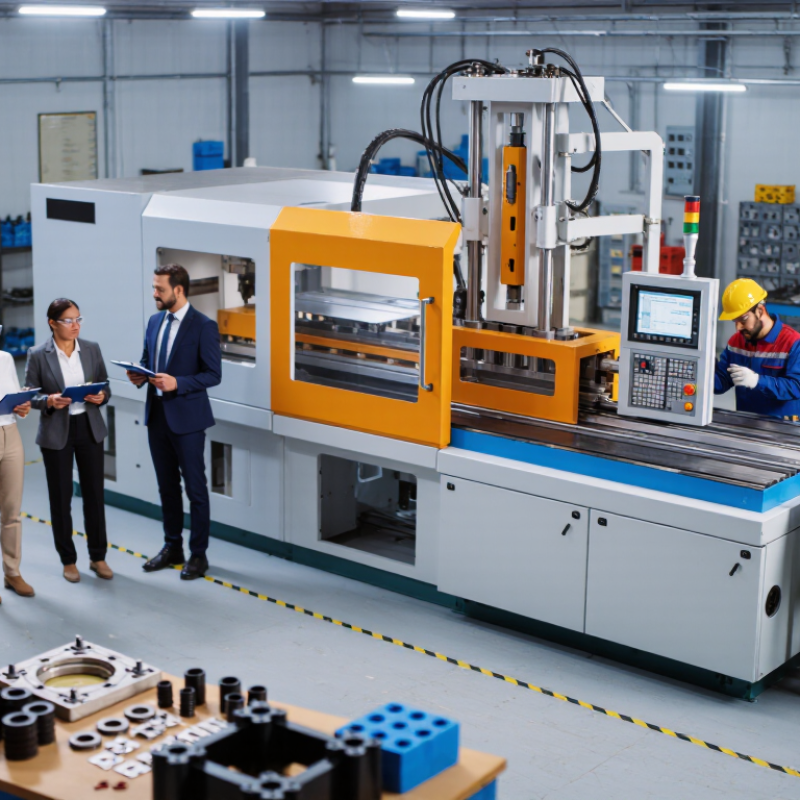
Rubber injection molding shapes uncured rubber by forcing it into a heated mold, where it cures into a solid part. The process can produce repeatable components at scale. Results still depend on the rubber compound, mold design, temperature, and cure time. A small change in wall thickness can affect how evenly material fills the cavity. Details matter.
Applications range from automotive seals and industrial gaskets to vibration mounts and protective boots. In each case, the part must suit its working conditions. A seal near hot machinery needs different heat resistance than a mount exposed to repeated movement. Medical components require careful material selection and application-specific validation. Buyers should also ask about tolerances, expected shrinkage, and inspection methods. A neat drawing may not show where flash could form or where a parting line might affect fit. No process removes every compromise; the best design often balances performance, tooling cost, and production volume.
10 Rubber Injection Molding Tips for Global Buyers - Understanding Rubber Injection Molding and Its Applications
| No. | Buyer Tip | What to Understand | Common Applications | What to Confirm with the Supplier |
|---|---|---|---|---|
| 01 | Define the part’s operating conditions | Temperature, pressure, movement, exposure to fluids, ozone, sunlight, and cleaning chemicals all affect elastomer selection and part design. | Seals, gaskets, vibration isolators, protective boots, and fluid-handling components. | Share the full service environment, expected lifespan, and any applicable performance requirements before requesting a quotation. |
| 02 | Choose the compound for the application | EPDM is commonly used for weather and water exposure; NBR is often selected for oil resistance; silicone is used where a broad temperature range or particular flexibility is needed. Suitability depends on the specific compound and conditions. | Weather seals, oil-resistant seals, appliance components, and temperature-resistant parts. | Request the compound designation, relevant test data, and confirmation that it is compatible with the actual media and operating conditions. |
| 03 | Distinguish rubber injection molding from liquid silicone molding | Conventional rubber injection molding commonly processes uncured rubber compounds that are heated and vulcanized in the mold. Liquid silicone rubber (LSR) uses a different metering and curing process. | Rubber seals and mounts; LSR keypads, flexible components, and selected medical or consumer parts. | Confirm the material form, molding process, curing method, and whether the supplier’s equipment is suitable for your chosen material. |
| 04 | Review the part design for moldability | Uniform wall sections, suitable radii, and a clear parting-line strategy can support more consistent filling and curing. Undercuts may require special mold features. | Custom grommets, diaphragms, seals, boots, and molded rubber-to-metal parts. | Ask for a design-for-manufacturing review covering parting lines, draft where relevant, undercuts, and likely areas of flash or trapped air. |
| 05 | Understand flash, parting lines, and trimming | Flash can occur where mold surfaces meet. Its amount and acceptability depend on the design, tooling condition, material, and agreed inspection criteria. | Precision seals, visible consumer components, and parts with tight mating interfaces. | Specify acceptable flash locations and limits, trimming method, and inspection approach on the drawing or quality agreement. |
| 06 | Agree on dimensions and tolerances early | Elastomers can deform under measurement and may change dimensions with compound, cure, geometry, and test conditions. A single tolerance should not be assumed suitable for every feature. | Sealing interfaces, press-fit components, and assemblies with defined compression or clearance. | Identify critical dimensions, measurement conditions, datum scheme, and the applicable drawing or industry standard before tooling approval. |
| 07 | Plan for tooling and production volume | Injection molding can support repeatable production, but mold design, cavity count, automation, and setup affect initial investment and unit economics. | Repeated production of seals, dampers, grommets, and other custom elastomer parts. | Compare tooling scope, expected tool life, maintenance responsibilities, cavity layout, sample stages, and pricing at realistic volume tiers. |
| 08 | Request evidence of process and quality control | Material traceability, controlled curing, dimensional checks, and documented inspection plans help manage consistency between production lots. | Automotive, industrial, appliance, and other applications with defined quality requirements. | Ask which inspection records, material certificates, sample approvals, and lot-traceability documents can be provided for your order. |
| 09 | Check chemical, regulatory, and market requirements | Requirements depend on the end use and destination market. Food-contact, drinking-water, medical, automotive, or electrical applications may require specific evidence or testing. | Food-contact seals, water-system components, medical devices, and electrical enclosures. | State the intended market and use, then verify applicable regulations, test methods, documentation, and whether the exact compound is covered. |
| 10 | Validate samples under realistic conditions | Visual inspection alone cannot establish long-term performance. Functional, dimensional, aging, compression, or media-compatibility tests may be appropriate for the application. | Critical seals, flexible joints, vibration-control parts, and components exposed to heat or chemicals. | Agree on sample quantities, acceptance criteria, test conditions, approval records, and the process for managing changes after approval. |
Related Posts
-
Exploring 2025 Top+ Rubber Injection Molding Innovations for Enhanced Production
-

Top 10 Benefits of Rubber Injection Molding for Your Manufacturing Needs
-
10 Best Rubber Injection Molding Techniques for Efficient Production?
-
Why Injection Molding is Essential for Modern Manufacturing Success
-
Why Choose a Plastic Extruder for Your Manufacturing Needs?
-
2025 Top 10 Innovations Revolutionizing the Injection Molding Process