7 Best Injection Molding Process Tips for Global Buyers

Choosing an overseas molding partner involves more than comparing unit prices. The injection molding process influences part quality, tooling life, delivery stability, and long-term production costs. A polished sample can still hide weak process controls.

John Bozzelli, a respected scientific molding consultant and founder of Scientific Molding, emphasizes, “You can’t inspect quality into a part; you must build quality into the process.” His point matters for global buyers. Quality should begin with mold-flow analysis, resin selection, drying conditions, and controlled machine settings. It should continue through first-shot approval and routine inspection.

Small details often decide the outcome. A damp nylon resin may create bubbles or brittle sections. Uneven cooling can leave sink marks beside a glossy surface. An unstable injection speed may produce visible weld lines from one batch to another. These problems are expensive after international shipment.

The following seven tips examine practical control points across the injection molding process. They cover design reviews, tooling communication, material documentation, trial validation, dimensional checks, and production monitoring. Buyers can use them when reviewing supplier records, asking technical questions, or comparing quotations.

No supplier is perfect. Some recommendations may need adjustment for medical, automotive, electronic, or consumer applications. Even experienced teams can overlook packaging pressure, regional standards, or temperature changes during transport. That is why reliable decisions require evidence, not confident promises. Ask for measurable data, clear acceptance criteria, and corrective-action records before placing a large order.
7 Best Injection Molding Process Tips for Global Buyers

Define Product Requirements Before Selecting an Injection Molding Method

Global buyers should define product requirements before selecting an injection molding method. Start with dimensions, wall thickness, weight, surface finish, and expected annual volume. Write them down clearly. A handheld enclosure may need a 1.5 mm wall, textured grip, and tight snap-fit tolerances. A storage component may prioritize strength and low tooling cost instead.

Material choice also shapes the process. Glass-filled polymers can improve stiffness, but they may increase wear on tooling and create visible flow marks. Flexible materials need different filling conditions than rigid engineering plastics. Thin walls may require higher injection pressure, while large flat parts can suffer from warpage. Material behavior matters.

Do not select a method from a sample photo alone. Ask for mold-flow analysis, dimensional studies, and details about cooling control. Confirm whether the supplier can maintain consistent temperatures, pressure, and cycle times across production sites. Request trial parts from the intended material and mold design. They reveal problems early.

Global projects also need defined inspection points, packaging conditions, and regional compliance requirements. Tolerances should reflect actual function, not ideal drawings. This is where teams often over-specify and raise costs unnecessarily. A pilot run can test assembly, color consistency, and shipping durability before full production. The best method is not always the fastest one.

Choose Suitable Materials, Molds, and Machine Specifications

7 Best Injection Molding Process Tips for Global Buyers

Choose materials with verified data, not attractive catalog claims. Check strength, heat resistance, shrinkage, moisture sensitivity, and surface requirements. A resin that works in one climate may fail after ocean transport. Dry moisture-sensitive materials before molding, and record drying temperature and time. Small records prevent expensive arguments later.

Match the mold design to the material and part geometry. Add suitable draft angles, balanced wall thickness, and cooling channels near thick sections. Poor cooling can leave sink marks, warping, or long cycle times. Confirm mold steel, cavity finish, gate location, and expected production volume with the supplier. Mold maintenance also matters. A clean vent can improve filling more than a higher injection speed.

Select a machine by clamping force, shot size, injection pressure, and screw diameter. Leave practical capacity, rather than running at the machine limit. Check whether the mold fits the platen, tie-bar spacing, ejector stroke, and controller requirements. Request trial samples under planned production conditions. Measure critical dimensions after cooling, not immediately after ejection. I still recheck shrinkage after several cycles. Early samples can look perfect.

A perfect choice is rare. Reliability comes from documented tests, clear tolerances, and honest communication.

Control Temperature, Pressure, Speed, and Cooling Conditions

Stable injection molding begins with controlled temperature, pressure, speed, and cooling. Measure the resin’s actual melt temperature, not only the machine display. A hot spot near the nozzle can cause degradation, flash, or inconsistent color. Keep the mold temperature within the material supplier’s recommended range. Small changes matter.

Set injection speed to fill the cavity smoothly without trapping air or creating jetting. A slower start may protect thin gates, while a faster middle stage can reduce premature freezing. Injection pressure should fill the cavity, but excessive pressure can increase stress and flash. Holding pressure then compensates for material shrinkage. Too much holding pressure may distort dimensions. Do not guess.

Cooling often determines cycle time and final accuracy. Check whether cooling channels cover thick sections, ribs, and corners evenly. Uneven cooling can produce warpage even when the part looks correct at ejection. Record coolant temperature, flow rate, and cooling time for every trial. Then compare part weight, dimensions, surface finish, and internal stress.

Global buyers should request process data, inspection results, and material traceability before approving production. A documented setting is more reliable than a verbal promise. However, one approved setting may not suit every cavity or seasonal factory condition. Revalidate after mold changes, resin changes, or extended machine downtime. That assumption fails.

Inspect Parts and Optimize the Process for Consistent Quality

7 Best Injection Molding Process Tips for Global Buyers

Inspect Parts and Optimize the Process for Consistent Quality

Consistent quality starts with physical inspection, not a supplier’s promise. Request first-article samples before approving mass production. Check critical dimensions with calibrated calipers, gauges, or a coordinate measuring machine. Inspect wall thickness, flash, sink marks, weld lines, and warpage under stable lighting. Record every measurement against the approved drawing and tolerance range.

Do not judge a part by appearance alone. A smooth surface can hide internal voids or uneven cooling. Review material certificates, dimensional reports, and production records for each batch. Ask how operators control mold temperature, injection pressure, holding time, and cooling time. Small changes can alter shrinkage and assembly fit. A process window should define acceptable settings, rather than relying on one “perfect” machine value.

Real production is rarely flawless. Even experienced teams may miss a slow temperature drift during a long run. That is why sampling plans and traceability matter. Inspect early, middle, and late production pieces, then compare the results. If dimensions move toward a tolerance limit, adjust the process before parts fail inspection. Keep records of corrections and repeat measurements after every change. Independent verification adds confidence for buyers working across borders. Still, reports need evidence. A polished document is not proof of control. Ask clear questions, inspect physical samples, and remain willing to revise the process when the data disagrees.

7 Best Injection Molding Process Tips for Global Buyers

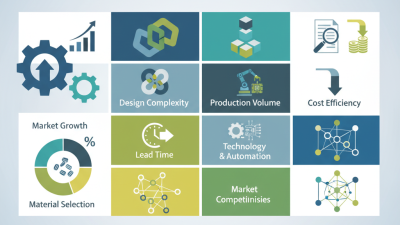
Inspect parts and optimize the process for consistent quality. The chart compares key quality-control practices by their typical priority in reducing molding variation.

How to use this chart: Prioritize process controls with higher quality impact, including mold temperature control, dimensional inspection, material drying, first-article approval, and continuous monitoring. Actual results vary by resin, part geometry, tooling condition, and production environment.

Manage Suppliers, Costs, Compliance, and International Shipping Risks

7 Best Injection Molding Process Tips for Global Buyers

Managing an injection molding project across borders requires more than comparing unit prices. Supplier capability, tooling control, resin traceability, and delivery reliability affect the real landed cost. The World Bank’s Logistics Performance Index 2023 shows significant differences in customs, infrastructure, and shipment tracking between markets. A low factory price may hide delays, rework, or expensive storage.

Tip: Request a costed quotation with resin grade, cycle time, cavity count, mold steel, inspection method, packaging, and Incoterms. Ask for recent process capability data, not only polished samples. During supplier audits, check drying systems, mold maintenance records, and measurement equipment. These details often reveal more than a sales presentation. I have seen buyers overvalue hourly rates while underestimating tool correction costs. That mistake is easy to repeat.

Compliance and shipping risks need equal attention. Confirm material declarations, product labeling, country-of-origin records, and required technical files before production. The WTO’s Global Trade Outlook and Statistics reported a 1.2% decline in merchandise trade volume during 2023, followed by projected growth in 2024. Demand can change quickly. Build contingency plans around ports, customs documents, and alternate production capacity. Tip: Approve a golden sample, retain mold ownership terms in writing, and use milestone inspections before shipment. Also test packaging under vibration and humidity conditions. It may feel excessive, but damaged goods create larger costs than preventive testing.