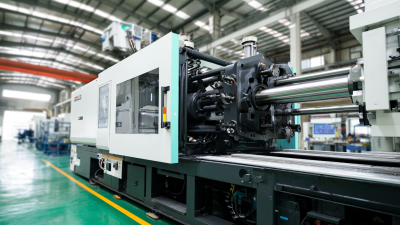
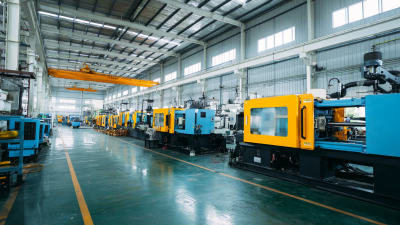
The 2026 plastic injection molding machine market is becoming more specialized, not simply larger. Manufacturers now compare hydraulic, all-electric, hybrid, vertical, two-shot, and multi-material platforms. Each type serves different production realities. A medical connector may require clean, repeatable electric motion. A large automotive panel may still need hydraulic clamping force. The correct choice depends on material, part geometry, cycle time, mold design, energy cost, and service access.
Industry reports show why this decision matters. PlasticsEurope’s Plastics—The Fast Facts 2024 reported global plastics production of approximately 413.8 million tonnes in 2023. Meanwhile, Fortune Business Insights’ 2024 Injection Molding Machine Market report forecast continued market growth through 2032. Estimates vary across research firms because they use different machine categories, regions, and revenue definitions. That difference deserves attention. No single number explains the whole market.
Energy efficiency is also changing purchasing decisions. Electric machines can reduce hydraulic oil use and improve motion control, especially during repetitive, high-volume cycles. Hybrid machines may offer a practical compromise for factories balancing capital cost and performance. However, lower energy consumption does not automatically mean lower total cost. Maintenance skills, spare-parts availability, mold changes, and downtime can change the final result.
This guide examines the leading machine types expected to shape 2026 purchasing decisions. It connects technical design with real factory conditions, including shot size, clamping force, precision, automation, and recycled-material processing. Some comparisons remain imperfect. Suppliers report performance differently. Buyers should test actual materials and molds before committing to a machine.
Plastic injection molding begins with small pellets poured into a hopper. A rotating screw moves them through a heated barrel. Friction and controlled heaters soften the material. The screw then pushes the melt into a closed mold under high pressure. After cooling, the mold opens, and ejector pins release the finished part. It looks simple. It is not always predictable.
Machine types mainly differ in their drive systems. Hydraulic machines use fluid power and remain useful for large molds and high clamping forces. Electric machines use servo motors, offering precise movement and lower idle energy use. Hybrid systems combine both approaches. According to PlasticsEurope’s Plastics—The Fast Facts 2024, global plastics production reached about 414 million tonnes in 2023. That scale increases pressure for accurate processing and reduced waste.
During a real production cycle, sensors monitor pressure, screw position, temperature, and cooling time. A slight temperature change can create a short shot, sink mark, or warped edge. The International Energy Agency identifies industrial motor systems as major electricity users, so machine efficiency deserves careful measurement. However, a lower energy reading does not guarantee better parts. Resin moisture, mold design, and operator settings can change the result. Factory teams often adjust holding pressure by a few seconds, then inspect the part under strong light. Data helps, but practical judgment still matters.
Plastic injection molding machines are commonly classified by their clamping mechanism: toggle, hydraulic direct, and two-platen systems. Toggle machines use linked arms to multiply force near mold closure. They are compact, fast, and suitable for high-cycle packaging parts. Hydraulic direct-clamp machines apply force through hydraulic cylinders. Their simple structure supports flexible mold changes, but energy use and oil maintenance require attention. Two-platen machines reduce machine length and work well with large molds. Their pressure balance can be impressive, although setup quality matters greatly.
Demand remains substantial. PlasticsEurope’s Plastics—The Fast Facts 2024 reports 413.8 million tonnes of global plastics production in 2023. That volume supports continued investment in molding capacity, but demand alone should not dictate machine selection. Grand View Research estimates the global injection molding machine market will expand through 2030, with automation and energy efficiency among key drivers. In practice, an electric or hybrid drive can reduce idle losses, while a hydraulic design may still offer better value for heavy-duty applications. The “best” mechanism is rarely universal. I would question any purchase based only on clamping tonnage.
Tips: Compare actual mold dimensions, cycle time, and pressure stability. Check platen deflection with your heaviest tool. Ask for measured energy data, not brochure estimates. A small toggle machine may outperform a larger hydraulic model on thin-wall parts, but poor maintenance can erase that advantage. Keep reviewing the decision after production begins.
2026 Top Plastic Injection Molding Machine Types: Types Classified by Drive and Power System
Plastic injection molding machines are often classified by their drive and power systems. Hydraulic machines use pumps, valves, and pressurized oil to generate clamping and injection force. They remain practical for large parts, deep molds, and demanding production cycles. Their strong force is useful. However, oil temperature can affect repeatability, energy use, and maintenance.
All-electric machines use separate servo motors for injection, clamping, metering, and mold movement. They provide precise position control, cleaner operation, and lower idle energy consumption. These advantages suit medical components, electronic housings, and thin-wall parts. Hybrid machines combine electric metering or injection with hydraulic clamping. They can balance precision, force, and investment cost. Servo-hydraulic systems improve traditional hydraulic control through variable-speed pumps. They often reduce wasted power, but results depend on correct sizing and tuning. No system is perfect.
Tips: Match the power system with your material, mold, cycle time, and factory conditions. Check peak load, not only average consumption. Measure oil temperature, recovery time, and part weight during trials. A small error in sizing can create a large monthly cost. I would not choose the lowest purchase price alone. Review maintenance skills, spare-part access, noise limits, and future production changes before selecting the machine.
Typical system-level energy-conversion efficiency ranges by drive architecture
All-electric machines generally achieve the highest energy efficiency because they transmit motion directly through electric servo motors. Servo-hydraulic and hybrid systems reduce power losses compared with conventional fixed-speed hydraulic designs, while actual performance depends on clamp force, cycle time, material, injection speed, and machine configuration.
The ranges are representative engineering values for comparison and are not brand-specific test results.
By 2026, the strongest injection molding choice will depend on the material and product, not machine size alone. Grand View Research estimates the global injection molding machine market will expand steadily through 2030, with energy efficiency remaining a major purchasing factor. Electric machines suit medical housings, electronic connectors, and thin-wall parts. They offer repeatable dosing and clean operation. Quiet cycles matter.
Hydraulic and hybrid machines remain practical for large automotive panels, crates, and thick structural components. They deliver high clamp force and tolerate demanding production schedules.
Two-shot machines support soft-touch grips, seals, and multicolor closures. Insert molding works well when metal pins or threaded components must become part of the finished product. For foamed interiors, specialized microcellular systems can reduce weight, but process windows are less forgiving.
Material selection changes the machine design. Silicone processing needs controlled temperature and metering. Recycled polymers often require stronger plasticizing units and better filtration. PlasticsEurope reported global plastics production at about 414 million tonnes in 2023, increasing pressure for efficient material use and recycled-content processing. The Plastics Industry Association also emphasizes contamination control as a key recycling challenge.
Small mistakes show quickly: silver streaks, black specks, or unstable weight. I have seen specifications look perfect on paper, yet cooling performance failed during extended runs. Machine selection still needs real mold trials, not only catalog data.
Choosing a plastic injection molding machine in 2026 starts with the application, not the machine’s advertised tonnage. A hydraulic machine suits demanding parts, recycled materials, and operations needing strong clamping force. An all-electric machine offers repeatable dosing, cleaner operation, and precise control for medical, electronic, or thin-wall components. Hybrid machines can balance energy use and force, but their performance depends heavily on configuration and maintenance quality.
Compare machines through real production conditions. Check shot size against the part weight, runner volume, and material density. Leave practical capacity, not excessive capacity. Match injection speed to wall thickness and filling behavior. A fast system may reduce cycle time, yet it can increase shear, flash, or cosmetic defects. Review platen dimensions, mold height, ejector stroke, and robot access before approving the machine. A machine that fits the mold poorly creates expensive delays.
Tips: Request trial parts using your actual resin and mold. Measure cycle stability over several hours, not just one successful shot. Check energy consumption per kilogram, noise, service access, and control-system records. Ask how quickly technicians can replace seals, heaters, or sensors. Smaller details matter. I have seen efficient machines underperform because operators could not reach critical components easily. That weakness is easy to overlook during a showroom demonstration. Also compare total operating cost, including training, downtime, tooling changes, and preventive maintenance. No machine wins every test.
| Machine Type | Typical Clamping-Force Range | Operating Characteristics | Energy-Use Profile | Repeatability and Process Control | Best-Fit Applications | Key Advantages | Important Limitations | Primary Selection Criteria |
|---|---|---|---|---|---|---|---|---|
| Hydraulic Injection Molding Machine | Approximately 30–6,000+ metric tons | Uses hydraulic pumps and valves to control clamping, injection, and auxiliary movements. Available in a very broad range of sizes. | Generally higher than electric systems because the hydraulic power unit may continue operating during idle periods. Variable-displacement pumps can reduce consumption. | Good process capability with modern closed-loop pressure, velocity, and position controls. Temperature and oil-condition management are important. | General-purpose production, large molded parts, automotive components, household products, and applications requiring high peak force. | Broad machine availability, strong force capability, suitability for large molds, and flexibility across many materials and part sizes. | Typically higher heat generation, more hydraulic maintenance, potential oil leakage, and less efficient idle operation than all-electric designs. | Required clamp force, injection rate, mold size, maintenance resources, cycle time, and total cost of ownership. |
| All-Electric Injection Molding Machine | Approximately 20–1,500 metric tons | Uses servo motors and ball screws or similar mechanical transmission systems for injection, clamping, and auxiliary movements. | Usually lower energy consumption, especially during standby and partial-load operation, because motors run mainly when motion is required. | Very high repeatability and precise control of position, velocity, pressure, and injection profile. Clean operation supports sensitive environments. | Medical parts, electronic components, precision packaging, optical parts, thin-wall products, and high-volume production. | High precision, fast response, low noise, clean operation, reduced hydraulic-fluid requirements, and efficient repeatable cycles. | Higher initial investment in many cases, more complex servo-drive service, and limited availability at the very largest clamp-force levels. | Required precision, cleanroom or contamination controls, cycle rate, energy price, service capability, and return on investment. |
| Hybrid Injection Molding Machine | Approximately 50–4,000 metric tons | Combines electric servo drives for selected movements with hydraulic systems for high-force or high-flow functions. | Often lower than conventional fixed-pump hydraulic machines while retaining hydraulic power where it is useful. | Good to very good repeatability, depending on the quality of the electric and hydraulic closed-loop controls. | Automotive parts, technical components, packaging, consumer products, and mixed production requiring a balance of performance and cost. | Balanced energy efficiency, force capability, speed, and purchase cost; suitable for a wide application range. | System architecture can be more complicated than a basic hydraulic machine, and efficiency varies by design and operating conditions. | Actual energy data at the intended cycle, control architecture, peak injection performance, service support, and component accessibility. |
| Vertical Injection Molding Machine | Approximately 15–1,500 metric tons | Typically uses a vertical mold-clamping arrangement. Some configurations include a vertical injection unit, while others use horizontal injection. | Depends mainly on the installed drive system; vertical orientation itself does not determine energy consumption. | Suitable for consistent molding when inserts are positioned accurately and the mold is properly supported. | Insert molding, overmolding, cable connectors, metal-plastic assemblies, small technical parts, and operations needing easy manual loading. | Convenient insert placement, reduced risk of inserts moving during mold closing, and good accessibility for certain assembly processes. | Usually requires more floor clearance; manual loading can reduce productivity and introduce variation if automation is not used. | Insert geometry, operator access, automation plan, safety guarding, mold layout, floor space, and required production volume. |
| Two-Platen Injection Molding Machine | Approximately 500–6,000+ metric tons | Uses two main platens and tie-bar or tie-bar-less clamping arrangements to provide high force with a relatively compact machine length. | Varies by hydraulic, hybrid, or electric drive package. Efficient pump control can reduce energy use during low-demand periods. | Good clamp-force control when platen parallelism, mold protection, and tie-bar strain monitoring are properly managed. | Large automotive components, pallets, containers, appliance housings, industrial parts, and large multi-cavity molds. | Compact length for its force class, large mold capacity, good accessibility around the mold, and suitability for large parts. | High capital cost, substantial installation requirements, and greater demands on foundation, utilities, and mold-handling equipment. | Part projected area, mold dimensions, mold weight, required injection volume, factory space, and installation infrastructure. |
| Micro Injection Molding Machine | Approximately 5–50 metric tons | Designed for very small shot sizes and small molds, often with specialized injection units for accurate metering of low material volumes. | Often efficient for small parts because the drive and heating systems are sized for low throughput, although performance depends on the machine design. | Can provide excellent repeatability when material drying, residence time, shot-size utilization, and mold temperature are tightly controlled. | Microfluidic components, miniature medical parts, laboratory products, small electronic components, and precision mechanisms. | Low material waste, accurate small-shot control, compact footprint, and suitability for miniature geometries. | Limited shot size, narrow process window, sensitivity to material residence time, and restricted compatibility with large molds or parts. | Minimum shot size, injection-unit resolution, material residence time, mold venting, part tolerance, and contamination control. |
| Multi-Component or Multi-Material Machine | Approximately 100–3,000 metric tons | Uses two or more injection units to mold different materials or colors in one cycle. Systems may use rotary, indexing, transfer, or sequential mold technology. | Usually higher than single-material molding because of additional injection units, mold movements, heating zones, and control systems. | High potential for repeatability, but synchronization, material compatibility, gate balance, and mold alignment are critical. | Two-color consumer products, soft-touch grips, seals, medical assemblies, automotive trim, and integrated multi-material components. | Eliminates secondary assembly steps, enables functional material combinations, and can improve product appearance and performance. | Higher mold and machine cost, longer setup, more complicated process development, and greater risk of material incompatibility. | Material bonding, shrinkage behavior, sequence control, mold technology, production volume, and cost of secondary operations. |
| High-Speed Packaging Injection Molding Machine | Approximately 100–1,000 metric tons | Optimized for short cycles, high injection speed, fast mold movements, and automated part removal or downstream handling. | Peak power demand can be high, but modern servo systems and optimized cycle profiles may reduce energy per part. | Requires stable high-speed control, accurate mold protection, reliable cooling, and consistent material drying. | Thin-wall containers, closures, caps, food packaging, healthcare packaging, and other high-volume products. | High output, short cycle potential, consistent part weights, and strong compatibility with automated packaging lines. | Higher mold and auxiliary-equipment requirements, narrower process margins, and increased sensitivity to cooling and material variation. | Parts per hour, injection speed, mold cooling capacity, automation synchronization, cavity count, and allowable wall thickness. |
| Foam or Structural-Foam Injection Molding Machine | Approximately 100–3,000 metric tons | Configured for processes that introduce a physical or chemical foaming agent to reduce density or create a cellular structure. | Energy use varies with material, shot size, injection method, mold temperature, and required pressure profile. | Requires precise control of melt temperature, gas or foaming-agent dosage, pressure history, and mold filling behavior. | Lightweight automotive parts, appliance components, protective housings, industrial products, and parts requiring improved stiffness-to-weight ratio. | Lower part weight, reduced material consumption, potential warpage reduction, and the ability to produce thicker sections. | Surface finish may require additional control, process development is specialized, and material or equipment compatibility must be verified. | Target density, surface-quality requirements, foaming method, material compatibility, mold design, and pressure-control capability. |